Strategic spare parts planning: how many is enough and why
Stocking too many spare parts can be a waste of funds and take up unnecessary storage. Too few spare parts in stock and an entire production line can come to a halt. Downtime increases as technicians wait for parts to be ordered to fix broken equipment.
Getting the balance right is critical for ensuring plants reduce downtime and keep costs manageable. It’s why strategic spare parts planning is such a valuable skillset. This methodology enables managers to budget the right amount of spare parts to reduce potential downtime and save on costs and wasted space.
For a broader look at maintenance approaches, see The complete guide to maintenance strategies in industrial automation.
What is strategic spare parts planning?
Strategic spare parts planning means deciding exactly how many spare parts to keep in stock. The goal is to keep machines working as much as needed, without spending more money than necessary.
These decisions are based on the type of part, how many are needed and where to store them. They also depend on how critical each machine is, how parts tend to fail and delivery times.
It applies predictive data and supply chain logistics to ensure parts are available exactly when a machine requires them. This approach evaluates asset risk profiles, component lifecycles and supplier lead times.
The cost of getting it wrong: stockout cost vs holding cost
Keeping spare parts in storage costs upfront money. But having no spare parts or not enough can cost even more down the line.
To get this balance right economically, the two opposing costs should be weighed up properly with the following considerations:
- The annual holding cost - This is usually between 20% and 30% of the part’s initial purchase value [1]. This percentage covers the cost of tied-up capital, warehouse floor space, insurance and physical degradation on the shelf. For example, electrolytic capacitors in programmable logic controllers (PLCs) degrade over time if left unpowered, turning poorly managed stock into unusable waste.
- The stockout cost - This is the total financial loss incurred while a machine sits idle waiting for a replacement part. According to the Society for Maintenance and Reliability Professionals (SMRP), total MRO inventory value should be no more than 1.5% of replacement asset value (RAV), with top-quartile performers falling between 0.3% and 1.5% depending on industry [2].
Failure of an essential component with no replacement parts on site increases the cost of associated downtime. The rushed shipping fees and potential emergency engineer call-out charges add to these costs.
Classifying spares by criticality: the ABC and XYZ framework
Tracking thousands of unique parts requires a structured categorisation matrix that combines financial value with demand predictability.
According to the Association for Supply Chain Management (ASCM), the ABC and XYZ classifications are core methodologies within supply chain performance management [3].
ABC analysis
This method divides the spare parts inventory into three distinct classes based on annual consumption value:
- Class A - High-value parts that make up roughly 70% of total inventory value but account for only 10% to 15% of physical stock. These items require strict tracking and low safety margins.
- Class B - Moderate-value items representing 20% of the financial value and 20% of the volume. These items use automated reorder points.
- Class C - Low-value components making up 10% of total value but 60% to 70% of the physical volume. These parts use bulk ordering methods like two-bin systems.
XYZ analysis
This framework can be combined with the ABC system to classify parts based on demand predictability:
- Class X - Constant and predictable demand. Sourcing these items is straightforward because failure rates follow regular patterns.
- Class Y - Fluctuating demand that follows production cycles or seasonal shifts.
- Class Z - Unpredictable demand with long periods of zero usage. This class often includes specialised automation assemblies and mechanical gearboxes.
When a manager combines these two frameworks into an ABC/XYZ matrix, procurement leads can better focus their capital. For example, an “AZ” part is costly and has unpredictable demand. You don’t want to spend funds buying the part for it to sit in storage and never be used. But you also don’t want to have to use a routine order through a supplier as it can take too long if an unpredictable event happens.
In this case, it makes more economic sense to have a supplier keep the part on hand instead of stocking it yourself.
Lead time risk as a strategic variable
According to the World Economic Forum's Global Value Chain Barometer, geopolitical disruptions to supply chains increased by 110% from December 2021 to January 2023. Climate-related risk events went up by 146% over the same time frame [4].
In terms of components, semiconductor lead times grew from 8-12 weeks in early 2020 to up to 52 weeks by late 2022 for some products [5]. A traditional approach assumes that a supplier will deliver a part within a fixed window. In reality, lead time variability can extend a typical two-week delivery out to several months.
If a factory relies on a single vendor with no local safety margins, any transport disruption halts production. Engineers must track worst-case supply windows rather than best-case scenarios when designing their storage protocols.

Calculating how many parts to hold
Teams can use the following standard formula to calculate the necessary safety stock for any given component:
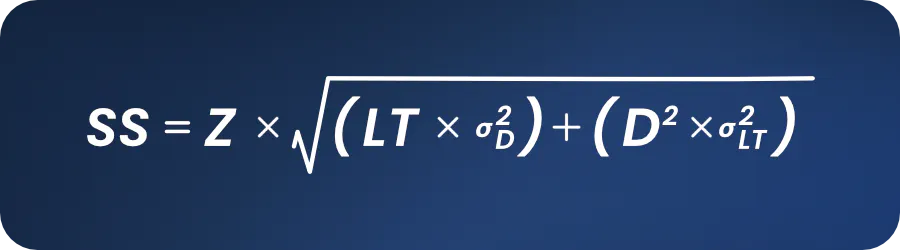
In this formula, Z represents the standard normal distribution factor for a target service level. LT is the average supplier lead time, and D is the average demand. The symbols σD and σLT denote the standard deviations of demand and lead time, respectively. Using this formula ensures that your stock buffers expand when a supplier shows unpredictable delivery habits [6].
If demand or lead times are highly variable, the required safety margins rise. When an item has a low stockout cost or a highly reliable supply chain, plants can safely lower their target stock volumes to free up capital.
Managing obsolete parts and legacy equipment
Heavy industry lines often rely on control systems that are decades old. Because industrial automation systems must outlast their original parts, operating and maintaining them with obsolete components is a challenge.
When an OEM discontinues support for a drive or controller, a standard procurement path disappears. Old equipment eventually needs replacement parts that are no longer made. As a result, plants often over-order these obsolete components from unverified sources. This choice increases the risk of receiving counterfeit or degraded hardware.
A more reliable alternative is to look at the entire legacy inventory and partner with EU Automation to stock remanufactured and certified parts. Sourcing through EU Automation allows plants to keep old machinery running without building costly on-site storage warehouses.
Sourcing via supplier-managed inventory and consignment stock
Plants do not need to own every part sitting in their warehouse. Alternative supply agreements let facilities reduce their capital exposure while having access to vital components when needed.
The following two approaches are used for expensive, slow-moving components, where carrying costs are very high but immediate availability is crucial:
- Consignment stock - The supplier owns inventory in a factory warehouse. The plant leader does not pay for it until it is used.
- Supplier managed inventory (SMI) - The supplier remotely tracks factory usage and automatically ships parts when required.
Connecting spare parts planning to broader maintenance choices
Different machine care programmes have different requirements for warehouse stock. A reactive maintenance system requires high volumes of unexpected spares because components are run to failure.
The ABB Value of Reliability survey found that 21% of businesses still rely on run-to-failure maintenance despite the high cost of unplanned outages [7]. This approach leads to disorganised storage and high shipping fees.
A preventive programme creates predictable batch demands, allowing teams to order components just before a scheduled shutdown. Advanced programmes like predictive maintenance and condition-based tracking alter the warehouse needs entirely. For example, when vibration sensors flag a bearing defect weeks early, the procurement team gains an extended window to source the exact part needed.
This early warning allows managers to order parts from external suppliers only when an alert occurs, reducing permanent storage costs.
Common pitfalls in maintenance inventory management
Many factories compromise their budget planning by falling into these inventory traps:
- Keeping duplicate records for identical parts because different technicians entered them under distinct manufacturer codes
- Stocking unnecessary spare parts for equipment that was replaced years ago
- Neglecting to control climate conditions in storage areas leads to rusted bearings
- Failing to update lead time records when a supplier shifts production facilities overseas
- Relying completely on an OEM for parts supply without evaluating third-party availability options
Key performance metrics for MRO inventory
Facilities should monitor these specific data points to track the health of their parts system:
- Inventory turnover ratio - The frequency with which your total stock is used and replenished over a year
- Stockout rate - The percentage of material requests that cannot be fulfilled immediately from available stock
- Service level - The probability that a part is available on the shelf when required for a repair
- Inactive stock percentage - The proportion of stored parts that have seen zero usage over a rolling 12-month window
Conclusion
Categorising items by their importance ensures that capital always covers true operational risks first. Accounting for shipping variations and outdated components prevents sudden production halts.
Plant leaders must link warehouse stock with modern tracking tools and a reliable supplier. This way, they can secure production targets while keeping budgets predictable.
For procurement teams who want to balance stockout risks with holding costs, EU Automation helps source current and obsolete spare parts, supporting the strategic planning of critical spares with short lead times and a global supply chain to help customers quickly access parts.
References
[1] Association for Supply Chain Management (ASCM), APICS Dictionary, 17th Edition, 2022.
[4] World Economic Forum / Kearney, Global Value Chain Barometer, January 2023.
[5] Simcona / Supply Chain Management Review, "Electronic Component Shortage Outlook," 2024–2025.
[6] Crack The Code - Understanding safety stock and mastering its equation
[7] ABB / Sapio Research, Value of Reliability Survey, 2023.