Hard-to-find and obsolete parts: how to source discontinued automation parts in 2026
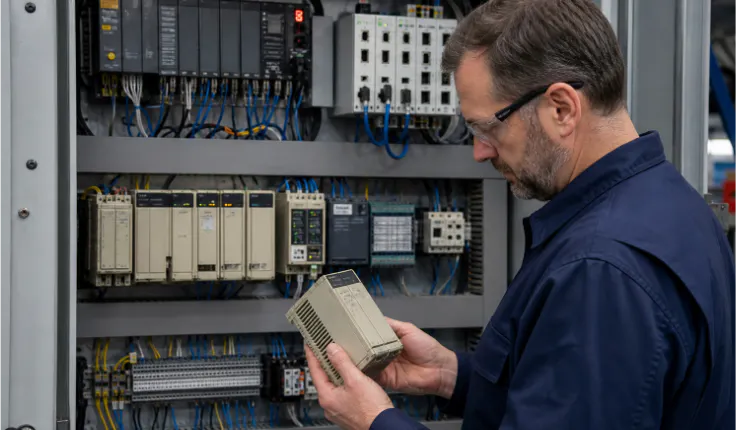
The part that finally stops a line is often the obscure module that went out of production years ago, bought once and forgotten until it failed. Around 473,000 electronic components reached end-of-life in 2023, and while that was down on the pandemic peak, hundreds of thousands of parts still drop out of production every year [1]. For plants running equipment built to last decades, sourcing obsolete parts is now a routine part of keeping production alive.
Many integrated circuits stay in production for only a few years, while industrial equipment is built to run for a decade or more [4]. That mismatch means a controller can be declared end-of-life long before the asset it controls is due for replacement. When such a part fails, there is no fresh stock to order, and the plant has to find a working unit on the secondary market or face an unplanned upgrade.
Sourcing a part that no longer officially exists is a particular skill, and the rest of this guide breaks it down. We cover what really counts as obsolete, the honest options once a part leaves the catalogue, the counterfeit traps waiting for an unwary buyer and the planning that stops the next end-of-life becoming a crisis. If you’d like the wider strategy first, from lead times to supplier risk, start with our complete guide to sourcing and managing automation components in a disrupted supply chain.
What makes a part obsolete?
A component is obsolete once its manufacturer stops making it. The international standard on the subject, IEC 62402, treats obsolescence as the point where an item can no longer be obtained from the people who originally supplied it, and lays out how organisations should anticipate and resolve that [2]. For a plant, the trigger is rarely convenient. It is usually a failed part and a supplier who no longer lists it.
Obsolescence does not always announce itself. Nearly a third of end-of-life events happen without a product change notice issued in advance, so the first sign a plant gets can be a failed order rather than a warning [1]. That is what makes obsolete parts so disruptive. The component was fine yesterday, and today it cannot be bought through normal channels.
It helps to separate the part from the asset. A drive, controller or I/O card reaching end-of-life is not a death sentence for the machine it sits in. What the plant has really lost is the easy route to a replacement, and the job becomes finding a sound unit by another path. Working out which parts have already gone, and which are close behind, is where a sensible response begins.
Why obsolete parts cost more than they appear to
Holding off and hoping a critical part lasts is usually the most expensive option of all. Once a component is discontinued, its price on the secondary market climbs steeply, and the cost of a forced redesign dwarfs the part itself. The main cost drivers are worth seeing plainly:
- Secondary-market premium - prices for chips after discontinuation generally run 10 to 15 times the original cost, turning a $3 part into a $30 relic, according to research from the University of Maryland's CALCE [4].
- Forced redesign - reworking a board or system around an obsolete part can cost anywhere from £20,000 to close to £2 million, depending on the component and the validation involved [1].
- Ongoing management overhead - obsolescence is a standing cost, not a one-off. CALCE found that a typical avionics manufacturer spends more than 10% of its annual component budget managing it [4].
Set against those figures, finding a discontinued unit to keep an asset working is almost always the cheaper answer. It also takes the panic out of any eventual upgrade, letting the plant choose when to modernise instead of being marched into it by a dead component.

Where to source hard-to-find and discontinued automation parts
A discontinued part still has three places it can come from, and your choice between them turns on how critical the asset is and how long the line can wait. The pressure to find hard-to-find parts is unlikely to ease, with average production-material lead times still running well above pre-2020 levels [5], so it pays to know the options before a failure forces a rushed decision. Our guide to [LINK: managing lead time in the supply chain] covers that side of the problem in detail.
Tracking down the original unit is the cleanest answer when it can be done. Nothing on the machine changes, no requalification is needed and the line goes straight back to how it ran before. Everything then hinges on finding a held unit that can actually be trusted.
Repairing or refurbishing the failed unit is the second option, and a good one for many assemblies. It tends to cost less than a new build, though it is slower, and it falls away the moment a part buried inside the unit has itself gone out of production.
Replacing the function with a current equivalent is the third path. Done deliberately, it ends the obsolescence problem for that part, but the engineering, downtime and revalidation it brings make it a project to schedule, not a fix to reach for in a breakdown.
The first of those routes is where sourcing gets delicate, because the market for legacy parts is wide, uneven and easy to get wrong. What separates a safe purchase is provenance: a seller who can prove where a unit came from and that it works. This is the gap EU Automation fills, holding discontinued automation parts that arrive documented and tested rather than as an unlabelled punt from an online listing.
Why are counterfeit parts a growing risk?
Counterfeiting is the hidden risk in obsolete sourcing, and it is getting worse. Reports of suspect parts hit a nine-year high in 2024, up 25% on the year before, and obsolete components made up the largest single share of those cases at nearly 43% [3]. Scarcity is exactly what counterfeiters exploit, because a buyer desperate for a discontinued part is less likely to ask hard questions.
The practical defence is provenance rather than price. Buying through EU Automation closes the gap counterfeiters rely on, because every unit’s origin and working condition are established before it ships.
Building an obsolescence management plan
Handling obsolete parts one crisis at a time is stressful and expensive. The alternative is to get in front of it with an obsolescence management plan. IEC 62402 sets out the principle: anticipate, assess and resolve obsolescence across an asset's whole life rather than reacting at the point of failure [2]. Such a plan can be light, but it has to be written down and revisited.
The work breaks into five steps:
- Build a parts list for the critical assets and mark anything already discontinued or nearing its end.
- Check manufacturer lifecycle status and field experience to spot the parts most at risk.
- Decide a route for each at-risk part: hold a spare, line up a specialist source, plan a repair path or schedule an upgrade.
- Hold spares of the most critical, hardest-to-find parts so a failure does not become an outage.
- Review the list on a fixed cycle, because a part that is current today can be discontinued without warning.
The aim is to turn obsolescence from a series of emergencies into a managed risk. A plant that knows which of its legacy parts are exposed can act before a failure, sourcing or stocking the awkward components while there is still time to choose. Our piece on obsolescence management in safety-critical sectors shows how the same discipline holds up where failure carries the highest stakes.
Conclusion
With hundreds of thousands of components reaching end-of-life every year and assets built to outlast the electronics inside them, sourcing discontinued parts is a normal demand on maintenance and procurement teams. The plants that handle it well treat it as a discipline. They know which parts are exposed, they buy from sources they can trust, they verify what arrives and they plan the next end-of-life before it lands. Handled that way, a discontinued component is an inconvenience to manage rather than a line stopped for weeks.
When a part becomes discontinued, EU Automation gives engineering teams a way to keep an ageing line earning. The module is found, checked over and shipped so production can carry on. It hands the timing of any modernisation back to the plant, to be taken as a considered call rather than a scramble triggered by a part nobody sells any more.
References
[1] Z2Data, Understanding Obsolescence in the Electronics Industry, 2024.
[2] IEC 62402:2019 Obsolescence management.
[3] ERAI / ASM International, Counterfeit Electronics Reports Reach Nine-Year High, 2025.
[4] CALCE, University of Maryland, Electronic Part Obsolescence (Life Cycle Mismatch).
[5] Deloitte, Restructuring the Supply Base: Prioritizing a Resilient, yet Efficient Supply Chain, 2024.